
A vessel is filling, a pump is running, and the control room display shows pressure climbing a little faster than expected. In many cases, the cause is routine: a valve is shut, a heat input has changed, or a downstream line is temporarily restricted. But pressure can rise from normal operating variation to a serious loss-of-containment hazard surprisingly quickly.
Process equipment is designed to contain pressure, not absorb unlimited pressure. Pipes, exchangers, reactors, storage tanks, columns, and separators all have mechanical limits established by their design and construction. Exceeding those limits can damage equipment, release hazardous material, and create conditions for fire, toxic exposure, or further equipment failure.
That is why pressure-relief systems are not simply emergency accessories. They are engineered safeguards that give excess pressure a controlled path away from protected equipment when normal controls, operating procedures, or isolation arrangements are not enough.
Understanding where overpressure comes from is a core chemical engineering skill. It connects thermodynamics, fluid flow, reaction engineering, process control, mechanical design, and plant operations into one practical safety question: if this equipment cannot relieve pressure normally, what credible event could make its pressure exceed its safe limit?
🔍 What “Overpressure” Actually Means
Overpressure occurs when the pressure inside equipment rises above the pressure it is intended to withstand under specified conditions. The relevant limit is often the maximum allowable working pressure (MAWP), a mechanical-design limit that depends on factors such as vessel geometry, material strength, wall thickness, corrosion allowance, joints, and design temperature.
Operating pressure is normally kept below this limit. A relief device is set to open before an unacceptable pressure is reached, subject to the applicable design rules and the system’s permitted accumulation during a relieving event.
📦 Why Contained Fluids Create Force
Pressure is force distributed over area. In a closed vessel, molecules collide with the walls; increasing the number of molecules, their temperature, or both increases the force exerted on the vessel.
A useful everyday analogy is a sealed aerosol can. Heating it raises vapor pressure even though no additional material is added. Industrial equipment behaves according to the same physical principles, but inventories, temperatures, stored energy, and consequences can be much larger.
⚖️ The Difference Between Design Pressure and Operating Pressure
Design pressure is selected for mechanical design; operating pressure is where the plant is intended to run. They are related but not interchangeable. A vessel may routinely operate well below its MAWP, while another may operate closer to it because the process requires elevated pressure.
Engineers need enough margin for normal fluctuations, but margin alone is not a protection strategy. A credible upset can exceed the margin, which is why relief design begins with identifying causes rather than assuming that routine operating distance from a limit is sufficient.
🌡️ Heating a Blocked-In Liquid
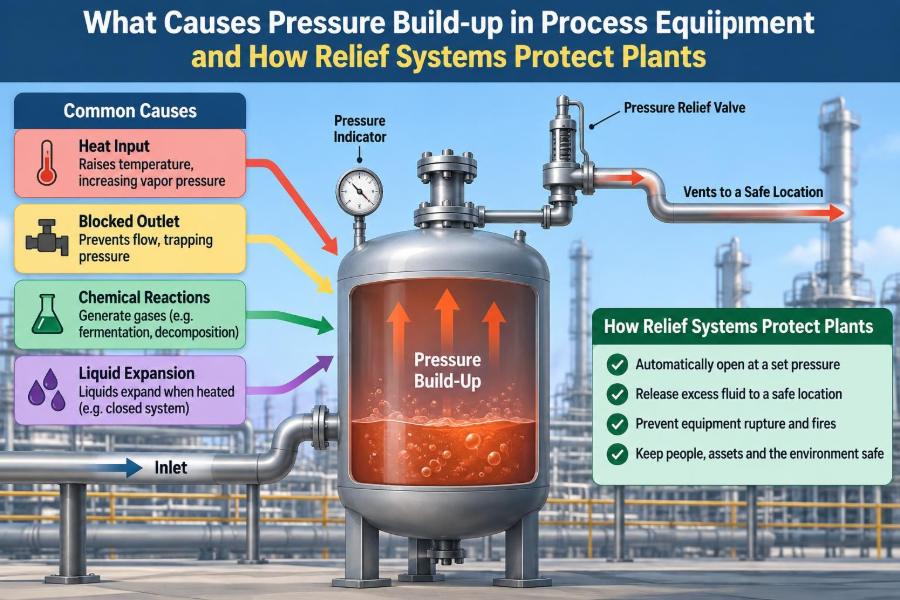
One of the most easily overlooked scenarios involves liquid trapped between two closed valves. Liquids are often treated as incompressible, but they still expand when heated. Because their compressibility is low, even modest thermal expansion in a completely filled, blocked-in line can generate very high pressure.
Sun exposure, steam tracing, a nearby hot process line, or changing ambient conditions can supply the heat. Small thermal relief valves are commonly used for this service, often returning liquid to a suitable closed system rather than discharging it to an open location.
🔥 External Fire and Heat Input
A fire near a vessel can heat its contents and metal shell. For vessels containing volatile liquid, heating can increase vapor generation and raise internal pressure rapidly. Fire may also weaken vessel material as temperature rises, reducing the mechanical strength available to resist pressure.
Fire relief sizing is therefore a distinct scenario in many relief studies. The required analysis depends on equipment configuration, wetted surface, insulation or fireproofing, drainage, fluid behavior, and the governing design basis. It should not be reduced to a generic rule of thumb.
🧪 Runaway Chemical Reactions
Exothermic reactions release heat. If cooling is lost, mixing becomes poor, reactants are charged too quickly, or an unintended reaction occurs, temperature can rise. Higher temperature can accelerate reaction rate, which releases still more heat: a feedback loop called thermal runaway.
Pressure may rise because of vaporization, gas formation, thermal expansion, or all three. Reactive relief design requires particular care because the discharged material may be two-phase, unstable, toxic, viscous, foaming, or capable of continuing to react after leaving the reactor.
💨 Gas Generation Inside Equipment
Some processes generate noncondensable gas through reaction, decomposition, corrosion, fermentation, polymerization, or contamination. Unlike a condensable vapor, a noncondensable gas cannot simply be condensed by modest cooling in a downstream condenser.
For example, an incompatible cleaning chemical accidentally introduced into a process vessel could produce gas. This is a hypothetical example, but it illustrates why relief scenarios must consider credible chemical incompatibilities, not only intended chemistry.
🚰 Liquid Filling and Pump Deadhead
A positive-displacement pump keeps displacing a nearly fixed volume per revolution. If its discharge valve is closed or downstream flow is blocked, pressure can rise until something yields, slips internally, or opens. A relief valve or bypass is usually essential on this type of pump discharge.
Centrifugal pumps behave differently: their flow falls as discharge resistance rises, and they have a finite shutoff head. Yet a blocked discharge can still overpressure lower-rated downstream equipment, cause overheating during prolonged no-flow operation, or worsen a process upset.
🚧 Blocked Outlets and Closed Valves
Equipment can become overpressured when material enters but cannot leave. The restriction might be a mistakenly closed manual valve, a failed control valve, a plugged line, a fouled filter, a closed isolation valve after maintenance, or an iced vent.
The engineering question is not merely whether a line exists on the drawing. It is whether every credible operating state leaves a reliable flow path. Valve lineups, lockout practices, bypass arrangements, and maintenance boundaries all affect that answer.
🔄 Reverse Flow From a Higher-Pressure Source
A low-pressure vessel connected to a high-pressure system can be exposed to reverse flow if a check valve leaks, an isolation valve is opened in the wrong sequence, or a pressure-control valve fails open. This is sometimes called high-pressure gas blowby when gas from the high-pressure side flows into lower-rated equipment.
Check valves reduce likelihood but are not automatically sufficient as the only safeguard. Their reliability, inspection history, potential for fouling, and the differential pressure involved must be evaluated in the specific service.
❄️ Condensation, Vacuum, and the Pressure Connection
Protection is often discussed as though pressure can only be too high. However, vessels can also collapse under external atmospheric pressure if internal pressure falls too low. Steam condensation in a blocked-in vessel is a classic mechanism: vapor condenses to liquid, its volume shrinks dramatically, and a vacuum can form.
Vacuum breakers, appropriately designed vents, and operating procedures may be needed. A pressure-relief valve is not necessarily a vacuum-protection device, so both directions must be considered separately.
🌊 Two-Phase Flow Makes Relief Harder
Relief systems are simplest when they handle a single gas, vapor, or liquid phase. Real upset conditions can produce a mixture of liquid and vapor. Flashing liquid, entrained droplets, foaming, and reaction-driven boiling can all create two-phase discharge.
Two-phase flow can alter capacity, generate large pressure losses, and create strong reaction forces in piping. Methods and assumptions used for sizing must match the expected behavior; treating a flashing reactive mixture as dry vapor can produce an unsuitable design.
🧭 Scenario Identification Comes Before Sizing
A relief valve cannot be selected intelligently until the plant understands what it must protect against. Relief studies usually consider causes such as blocked discharge, control-valve failure, utility failure, exchanger tube rupture, fire, thermal expansion, reaction, and inadvertent valve opening.
Not every imaginable event must be combined. The task is to identify credible scenarios, determine which can occur together, and calculate the required relieving load for the governing case. This structured reasoning is more valuable than starting with a valve catalogue.
📋 A Simple Scenario Screening Framework
For each protected item, engineers commonly ask a sequence of practical questions:
- What can enter the equipment, and at what maximum rate?
- What can add heat, generate gas, or vaporize liquid?
- What outlet or vent path could become unavailable?
- What is the equipment’s pressure and vacuum rating?
- Which independent safeguards prevent the event, and which only mitigate it?
- Where will relieved material go, and can that destination handle it?
The answers should be documented with process data and defensible assumptions. A relief calculation is only as credible as the scenario definition behind it.
🛠️ What a Pressure Relief Valve Does
A pressure relief valve opens automatically when inlet pressure reaches its set pressure. Its purpose is to pass enough fluid to limit pressure rise within the allowed range during the selected contingency.
Spring-loaded valves are common. Pressure acting on the valve disc overcomes spring force, lifting the disc and creating a flow area. The valve reseats as pressure falls, although actual opening and closing behavior includes blowdown and depends on valve design and service conditions.
🧰 Other Devices in the Relief Toolbox
A relief system may use devices other than a conventional spring-loaded valve. The choice depends on fluid properties, tightness requirements, process pressure, fouling tendency, response needs, and disposal arrangement.
| Device | Typical role | Key consideration |
|---|---|---|
| Spring-loaded relief valve | Automatic overpressure protection | Backpressure and service compatibility can affect performance |
| Rupture disk | Opens by bursting at a specified differential pressure | Single-use device; burst tolerance and installation matter |
| Pilot-operated valve | High-capacity or close-set pressure service | Small pilot lines must remain reliable and clean |
| Conservation vent | Low-pressure tank breathing service | Not a substitute for emergency venting where required |
| Vacuum relief device | Protects against excessive vacuum | Must be sized for credible inbreathing demands |
💥 Rupture Disks: Useful but Not Universal
A rupture disk is a thin, engineered membrane that bursts when its specified pressure differential is reached. It can provide very rapid opening and is useful where a valve might stick, where absolute leak tightness is needed, or where corrosive or polymerizing process fluid should be isolated from a relief valve.
Its limitations matter too. Once burst, it stays open and must be replaced. A disk installed upstream of a relief valve can create a small trapped space that needs monitoring, and its effect on the combined device capacity must be considered.
📏 Set Pressure, Accumulation, and Blowdown
Set pressure is the inlet pressure at which a relief device is intended to begin opening under defined test conditions. During a real event, pressure may rise above set pressure while the device reaches sufficient lift and flow. That increase is called accumulation, while overpressure is often expressed relative to set pressure.
Blowdown is the difference between set pressure and reseating pressure. These terms are easy to confuse, but they describe different parts of valve behavior. Applicable codes and company practices define acceptable limits for particular equipment and scenarios.
📐 Sizing Is About Required Flow, Not Valve Diameter
A large-looking valve is not necessarily adequate, and a small one is not necessarily inadequate. Sizing begins by estimating the required relieving rate, then determining the certified effective area and configuration needed to pass that rate at relieving conditions.
Fluid molecular weight, temperature, compressibility, latent heat, density, viscosity, inlet losses, and backpressure can all matter. The calculation method changes substantially between gas/vapor, liquid, and two-phase service. Qualified engineers use recognized methods, verified data, and device-specific certified capacity information.
🧱 Inlet Piping Can Undermine a Good Valve
The relief valve only senses pressure at its inlet. If inlet piping is long, narrow, or full of restrictive fittings, pressure loss can cause unstable valve operation, including chatter. Chatter damages seating surfaces and can reduce reliable capacity.
Good layouts aim for a short, direct inlet connection with suitable geometry and no unnecessary restrictions. This is not a drafting detail: piping configuration is part of the protective function.
🌪️ Backpressure Changes Valve Behavior
Pressure at a relief valve outlet is called backpressure. It may come from a flare header, vent line, scrubber, knockout drum, or other common disposal system. Built-up backpressure develops as flow moves through downstream piping; superimposed backpressure may already exist before the valve opens.
Excessive backpressure can reduce capacity or change the opening behavior of some conventional valves. Balanced bellows valves and pilot-operated designs can help in suitable applications, but each introduces its own inspection and failure considerations.
🏭 Relief Is Only Half the System
Opening a valve removes pressure from the protected equipment, but it transfers mass and energy somewhere else. The discharge route must safely contain, separate, burn, scrub, recover, or otherwise manage the relieved material.
A flare system, for example, may include relief headers, knockout capacity to remove entrained liquid, a seal or purge arrangement, and a flare stack. Its performance must be assessed for coincident loads where credible; protecting one vessel must not overload the common destination.
🧯 Choosing a Safe Disposal Route
Atmospheric discharge may be appropriate for some benign fluids in a safe location, but it is not a default answer. Toxic, flammable, environmentally harmful, hot, or oxygen-displacing releases often require a closed disposal system or treatment step.
Disposal design must also account for noise, reaction forces, cold temperatures from flashing, liquid carryover, ignition sources, personnel access, and the possibility that a discharge creates a hazardous vapor cloud. A relief valve that opens successfully can still create danger if its outlet system is poorly designed.
🧩 Layered Protection Before Relief Opens
Relief devices are usually a final automatic layer, not the preferred means of routine pressure control. Plants first use sound process design, controls, alarms, operator response, interlocks, trips, isolation, and operating procedures to keep the process within normal limits.
These layers have different functions. A pressure controller may correct a normal disturbance; a high-pressure trip may stop a feed; a relief valve limits pressure if those measures fail or respond too slowly. Independence matters: two safeguards sharing the same sensor, utility, or failure mode may not provide the expected protection.
👷 Operations Practices That Prevent Overpressure
Many pressure incidents begin with ordinary activities: startup, shutdown, line clearing, maintenance isolation, cleaning, or switching to a spare pump. Clear procedures should identify venting, draining, valve positions, pressure equalization, and the sequence for opening connections between systems at different pressures.
Operators also need to recognize abnormal trends. A slowly rising pressure may signal fouling, a blocked vent, unwanted heating, or a control problem long before a relief device is challenged. Treating repeated relief lifting as “normal” is a warning sign, not a stable operating practice.
🔧 Inspection, Testing, and Mechanical Integrity
Relief devices can corrode, foul, leak, stick, lose set-pressure accuracy, or be installed incorrectly. Inspection and testing programs are therefore central to mechanical integrity. The appropriate interval and method depend on service severity, device type, process history, regulatory requirements, and site procedures.
Equally important are practical checks: Is the inlet isolation valve locked or sealed open where required? Is the discharge path clear? Has a rupture disk been replaced with the correct specification? Has a maintenance change altered the protected equipment or its scenario?
📝 Management of Change Protects the Original Design Basis
A relief system is designed around a particular process basis. Changing feed composition, raising utility pressure, adding insulation, debottlenecking a pump, revising control logic, or routing a discharge to a new header can invalidate earlier assumptions.
Management of change should trigger review when modifications affect pressure sources, heat input, relieving rates, set points, backpressure, materials, or disposal capacity. The drawing may still look familiar while the actual risk has changed.
⚠️ Common Mistakes in Relief-System Thinking
- Using a valve size copied from similar equipment: similar appearance does not prove similar relieving duty.
- Ignoring blocked-in liquid: small piping segments can require thermal relief.
- Counting a check valve as infallible: it can leak, stick, or be bypassed by an operating error.
- Focusing only on the valve: inlet losses and outlet backpressure can control performance.
- Assuming a flare has unlimited capacity: common headers need system-level analysis.
- Forgetting vacuum: an atmospheric-pressure vessel can fail inward as well as outward.
🧠 A Practical Way to Read a Relief P&ID
When reviewing a piping and instrumentation diagram, trace the protected equipment, its pressure sources, the relief-device inlet, any isolation valves, and the final disposal destination. Then ask what happens if each major control valve fails, each utility is lost, or a connecting valve is opened.
Also compare the drawing with field reality. Temporary hoses, spectacle blinds, altered drain routes, missing supports, and unofficial valve lineups can create conditions that are absent from the original design documents.
📚 Codes, Standards, and Engineering Judgment
Pressure-relief design is governed by applicable codes, regulations, company standards, and recognized engineering practices. These establish requirements for equipment construction, device selection, testing, installation, and documentation. Their exact application varies by jurisdiction, equipment type, and service.
Standards do not eliminate judgment. Engineers still need sound process data, realistic scenarios, clear assumptions, and review by people who understand operations, metallurgy, reaction hazards, and disposal systems. Complex reactive or two-phase cases may require specialist analysis.
🧪 Worked Thought Experiment: A Heated Isolated Line
Imagine a short line full of liquid solvent between two closed block valves. The line is near hot equipment, and the sun or process heat raises the liquid temperature over several hours. There is no gas pocket and no place for the expanding liquid to go.
The pressure rise is not limited by the line’s small volume. It is governed by liquid thermal expansion and the stiffness of the confined system. A correctly located thermal relief valve can return the small expansion flow to a lower-pressure closed system. Simply assuming “the line is too small to matter” would miss the mechanism.
✅ The Core Principle: Give Pressure a Controlled Path
Every overpressure problem has two parts: a source that adds mass or energy, and a limitation that prevents the system from accommodating it. Heat, reaction, incoming flow, reverse flow, and trapped liquid are sources; closed valves, restrictions, failed controls, and inadequate disposal paths are limitations.
Reliable pressure protection comes from identifying credible sources, limiting them where possible, and providing a verified path that can safely handle the remaining load. The relief device is vital, but it works only as part of an integrated system of equipment design, controls, piping, disposal, inspection, and disciplined operation.
Pressure relief is not about expecting equipment to fail; it is about ensuring that foreseeable upsets release energy and material in the safest controlled way available. That mindset turns a valve on a drawing into a complete plant-safety function. 🧯🏭⚙️